
Preparation and alignment
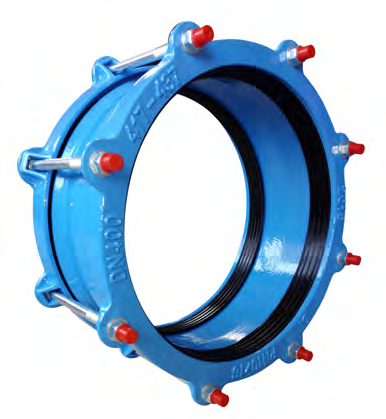
Examine both pipe ends
Ensure the pipe ends are round, smooth and free from bulges, dents, score marks, scale, rust and loose debris. Check that both pipe diameters are within the range provided for the coupling. Weld beads must be ground flush while maintaining the correct surface profile.
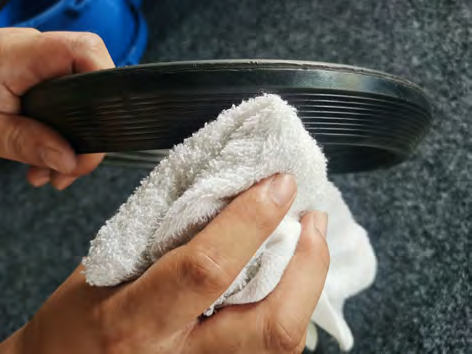
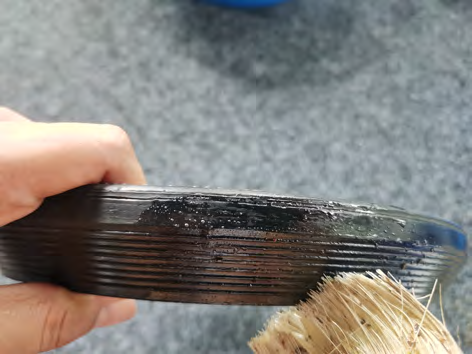
Check the gasket and lubrication
Check that the grade of gasket is suitable for the conveyed medium. Check that the rubber seal is sufficiently lubricated where it contacts the coupling centre barrel. If not, apply a suitable lubricant.
Align, support and mark
Align the pipe to be laid with the pipe already in position. Keep the pipe ends concentric, adjusting the support or trench bed as necessary. Mark both pipe ends at a distance equal to or greater than half the overall assembled width of the coupling. Place the coupling wholly on one pipe end.
Tightening and setting gap
Centre the coupling
Adjust the setting gap between pipe ends as necessary. Using the marks made in Step 3, slide the coupling to a central position over the pipe ends and commence bolt-up.
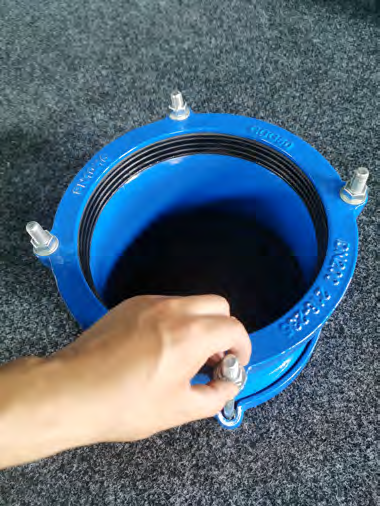
Tighten opposite bolts progressively
Tighten diametrically opposed bolts, giving the nuts one or two turns at a time to draw up the end rings evenly. Tighten to the specified torque, working around the coupling as many times as necessary. The radial gap between the pipe and coupling should be even all the way round. Rubber may be seen to extrude.
Bolt torque rating
| Bolt size | Torque (Nm) |
|---|---|
| M12 | 70–80 |
| M14 | 90–100 |
| M16 | 100–120 |
Tighten in diametrically opposite pairs. The source torque section specifies 2 or 3 turns per pass; installation Step 5 specifies 1 or 2 turns. Confirm the applicable tightening procedure for the supplied assembly.
Setting gap reference
| Coupling DN (mm) | Sleeve width (mm) | Recommended gap (mm) | Max. gap (mm) |
|---|---|---|---|
| Up to DN200 | 100 | 16 | 32 |
| Over DN250 – DN700 | 160 | 20 | 40 |
| Over DN700 – DN1600 | 200 | 20 | 40 |
The source gap table extends beyond this guide’s stated DN40–DN600 size range and leaves the interval above DN200 through DN250 unclear. Its sleeve widths must not be equated automatically with the L column in the size table. Confirm the applicable row and pipe-end gap for the exact coupling.
Size reference
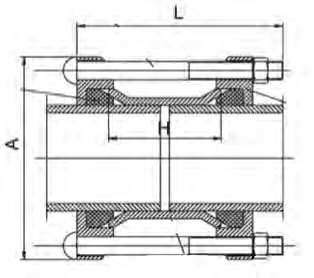
Size and range reference
| SIZE | RANGE | A | L | L | Qty |
|---|---|---|---|---|---|
| DN40 | 48-63 | 165 | 100 | M12*180 | 2 |
| DN50 | 59-72 | 180 | 95 | M12*180 | 2 |
| DN65 | 72-85 | 180 | 95 | M12*180 | 3 |
| DN80 | 88-103 | 190 | 95 | M12*180 | 4 |
| DN100 | 93-117 | 200 | 95 | M12*180 | 4 |
| DN100 | 107-128 | 214 | 95 | M12*180 | 4 |
| DN125 | 138-153 | 250 | 95 | M12*180 | 4 |
| DN150 | 155-175 | 278 | 105 | M12*200 | 4 |
| DN150 | 159-182 | 278 | 105 | M12*200 | 4 |
| DN175 | 192-210 | 300 | 130 | M12*220 | 4 |
| DN200 | 218-235 | 324 | 130 | M12*220 | 4 |
| DN225 | 250-267 | 406 | 130 | M12*230 | 6 |
| DN250 | 235-252 | 406 | 130 | M12*230 | 6 |
| DN250 | 271-289 | 440 | 130 | M12*230 | 6 |
| DN300 | 315-332 | 452 | 130 | M12*230 | 6 |
| DN300 | 322-339 | 463 | 130 | M12*230 | 6 |
| DN300 | 324-350 | 510 | 165 | M12*230 | 6 |
| DN300 | 345-375 | 510 | 165 | M12*230 | 6 |
| DN350 | 374-391 | 510 | 165 | M16*250 | 8 |
| DN400 | 400-429 | 560 | 165 | M16*250 | 8 |
| DN400 | 417-437 | 560 | 165 | M16*250 | 8 |
| DN400 | 455-472 | 560 | 165 | M16*250 | 8 |
| DN450 | 480-500 | 560 | 165 | M16*250 | 8 |
| DN500 | 500-535 | 560 | 165 | M16*250 | 8 |
| DN500 | 526-546 | 630 | 165 | M16*250 | 8 |
| DN500 | 555-572 | 700 | 165 | M16*250 | 10 |
| DN600 | 600-630 | 700 | 165 | M16*250 | 10 |
| DN600 | 630-650 | 700 | 165 | M16*250 | 10 |
Both L headings are retained as printed. The first L column contains numeric values; the second contains bolt designations such as M12*180. Do not treat them as the same dimension. Confirm the current drawing, symbols and units before dimensional use.
Keep the matching document with the product.
Use the guide for the supplied configuration. For project-specific requirements, contact aquafitting@gmail.com and quote AQF-IG-UC-001.